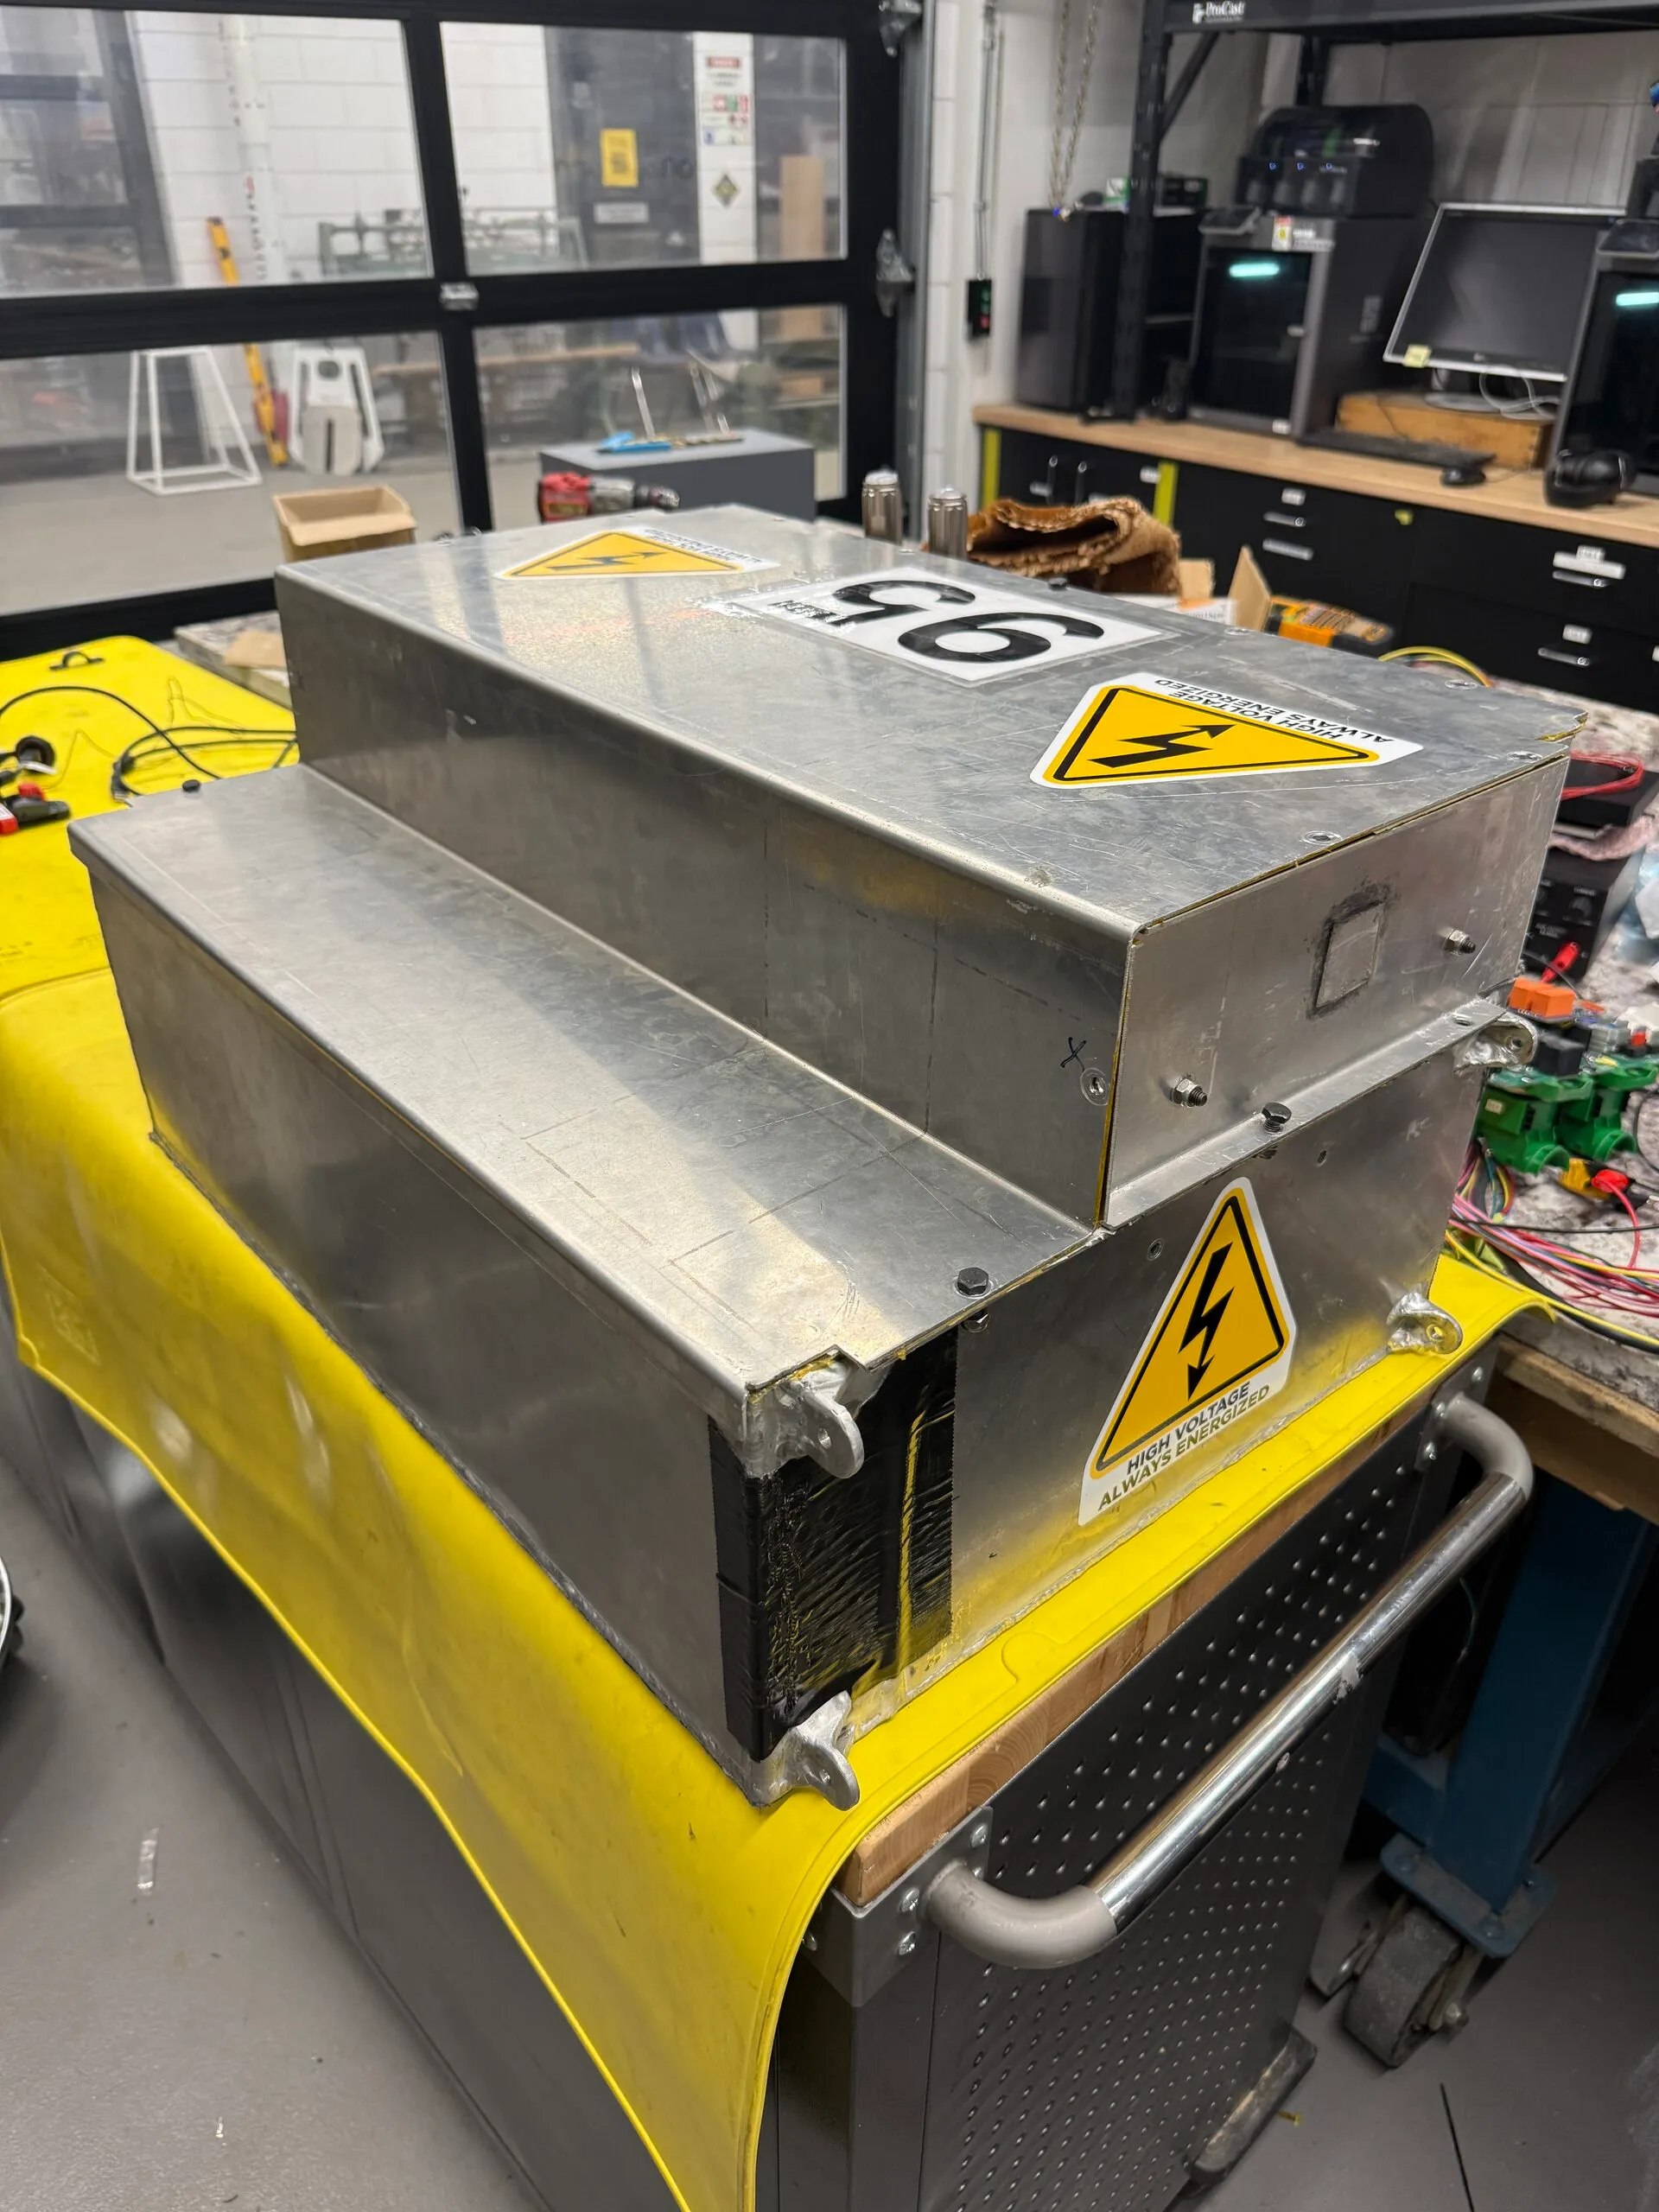
Building the Accumulator, Safely
Manufacturing the HV accumulator: qualifying every cell through tab testing, assembling segments, the BMS bring-up, and the harnessing and safety discipline that a 400V pack demands.
The accumulator is the densest concentration of energy, cost, and risk on the car, and building one is as much about process as it is about parts. This entry covers how we manufacture the pack: qualifying cells, assembling segments, and the high-voltage safety habits that make it routine instead of scary.
Qualifying every cell
Before a cell earns a spot in the pack, its tabs get tested. Our tab testing procedure puts each connection under a high current load while we watch for voltage drop and heating, because a weak joint that survives the bench will not survive an endurance run.
To make the data trustworthy I wrote a Python script that reads current measurements from the high current supply through an ADC, logging every test so a marginal tab is a number in a spreadsheet, not a judgment call at the bench.
Segment assembly
Cells stack into segments with the monitoring hardware built in from the start: thermistors placed where the pack needs watching, and sense leads dressed away from power paths so the BMS wiring stays short and serviceable. Torque values get written down and checked, because a loose busbar connection is a hot spot waiting for competition.
HV and LV harnessing
Wiring the pack is two disciplines in one box. The HV side is busbars, maintenance plugs, and the interlock loop, routed with creepage and clearance in mind. The LV side is the BMS sense and isoSPI network, kept physically separated from HV runs so a chafed wire can never bridge the two. Everything is labeled and strain-relieved before the lid goes on, since the inside of a sealed accumulator is the last place you want a mystery.
Commissioning the BMS
A pack is not done when the lid closes; it is done when the BMS agrees. Each centralized CAN group module gets its firmware checked and flashed to a common version, then addressed and configured so the master has a clean picture of every segment. The CAN module log is the record that all of them answered.
Only then does the pack get its first controlled energize: precharge, contactor close, and a full sweep of cell voltages and temperatures read back over CAN against what a handheld meter says at the taps.
Working at 400 volts
The rules that keep the team safe are boring on purpose:
- The pack is treated as live until it is measured dead. Verify with a meter, not with an assumption.
- Insulated tools, HV gloves, and a second person present for any energized work.
- Contactors, precharge, and the insulation monitoring device stay in the loop during every test. Bypassing safety hardware to save time is how teams end up on the news.
- The BMS gates the contactors: over-voltage, under-voltage, or over-temperature on any cell opens the pack, no exceptions.
The payoff of all this discipline is trust. A pack whose every cell has a test record and whose every connection has a checklist behind it is a pack the whole team can work on without fear, and that trust is what lets an electric car program move fast.